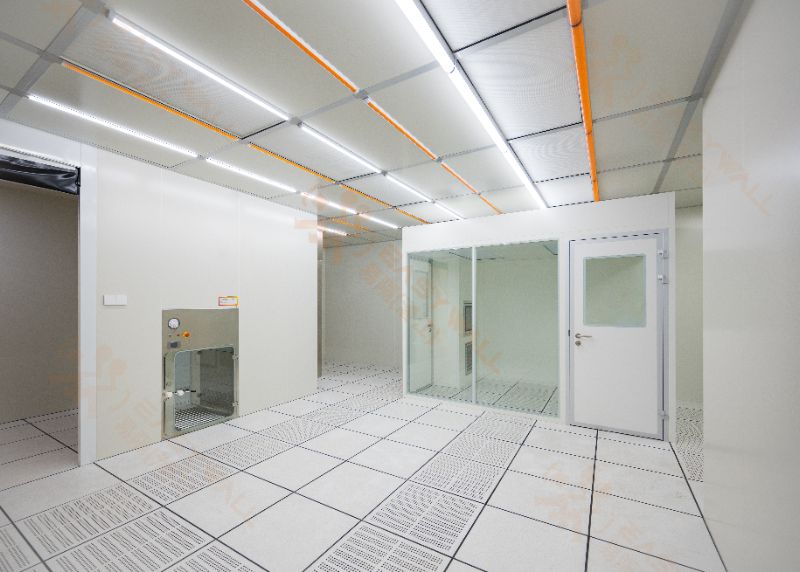
A GMP-friendly cleanroom panel is smooth, non-shedding, non-porous, chemically compatible, durable, sealed at joints and penetrations, fire-rated where required, and supported by documented testing and validation. I evaluate the complete wall or ceiling assembly—not only the facing material—because contamination control depends on the panel core, joints, interfaces, installation, cleaning program, HVAC pressure control, and maintenance records.
In pharmaceutical manufacturing, GMP-friendly cleanroom panels provide the physical enclosure needed to control particles, microorganisms, moisture, cleaning chemicals, and airflow leakage. They do not create GMP compliance by themselves. Instead, they support compliance when the full facility is designed, installed, qualified, operated, and maintained according to the applicable GMP, ISO, FDA, EU GMP Annex 1, fire-code, and project requirements.
!
Before I select a panel system, I define the room classification, manufacturing process, cleaning chemicals, temperature range, humidity level, pressure cascade, fire strategy, and expected maintenance frequency. I also identify whether the room is used for dispensing, formulation, aseptic processing, packaging, laboratory testing, or support operations. Each activity can impose different requirements on cleanroom wall systems.
The project specification should identify the required ISO classification, GMP grade where applicable, surface finish, panel thickness, core material, joint design, fire rating, thermal performance, and service-life expectations. For pharmaceutical facilities, I also require coordinated drawings showing doors, windows, pass boxes, return-air openings, utilities, lighting, sprinkler heads, and process equipment. This reduces uncontrolled cutting and sealing during installation.
A supplier’s statement that a product is “GMP compliant” is not enough evidence. I look for technical datasheets, material declarations, fire-test reports, chemical-resistance information, dimensional tolerances, installation procedures, cleaning instructions, and quality-control records. The final compliance position must be confirmed through the completed room and its qualification documentation.
The interior surface is the first barrier against contamination accumulation. I specify a continuous, low-porosity finish that can tolerate the approved cleaning and disinfection program without blistering, cracking, chalking, corrosion, or color transfer. The surface should not shed fibers, flakes, particles, or coating fragments during normal use, cleaning, or minor contact with carts and equipment.
A useful specification should replace vague terms such as “smooth” with measurable acceptance criteria. For example, the project can define a maximum surface roughness value, allowable waviness, coating thickness, gloss range, color tolerance, or visual defect limit. The selected limits must match the process risk and cleaning method rather than being copied from an unrelated facility.
Common surface options include stainless steel, coated steel, galvanized or pre-painted steel, HPL, fiberglass-reinforced plastic, and specialized composite boards. Stainless steel is frequently selected for aggressive cleaning, frequent washdown, and corrosion-sensitive areas, while HPL can provide a durable hygienic finish for many pharmaceutical and laboratory interiors. Coated steel may be suitable where the coating system has documented chemical compatibility and the room does not expose the surface to unsuitable solvents or concentrated disinfectants.
There is no single best material for every GMP application. The appropriate choice depends on disinfectant exposure, impact risk, humidity, fire requirements, cleaning temperature, thermal cycling, and the required service life.
| Material or core | Typical benefit | Selection concern |
|---|---|---|
| Stainless steel facing | Corrosion resistance and frequent-cleaning capability | Higher material cost, potential denting, and joint detailing |
| HPL facing | Durable, cleanable, and available in multiple finishes | Chemical compatibility and edge-sealing details must be verified |
| Coated steel | Broad availability and controlled surface finish | Coating damage can expose the substrate |
| Fiberglass or FRP | Moisture and corrosion resistance | Surface repair and compatibility with disinfectants require review |
| Rock wool core | Fire performance and acoustic insulation | Weight, moisture control, and edge protection |
| PIR or PU core | Thermal insulation with lower panel weight | Fire classification and smoke performance must be documented |
| EPS core | Cost-effective insulation for selected applications | Fire-code acceptance and process suitability may limit use |
| Aluminum or paper honeycomb | Lightweight and rigid construction | Fire behavior, edge closure, and structural loading require review |
The core is not directly exposed to the cleanroom in a properly sealed assembly, but it still affects fire performance, insulation, panel deflection, acoustic behavior, weight, and installation. I avoid selecting a core based only on price because a low-cost option may create additional fire protection, reinforcement, or replacement requirements. For pharmaceutical cleanrooms, the core and facing must be evaluated as one tested system.
Panel surfaces cannot support contamination control if the joints collect dust or allow air movement through the enclosure. I specify flush-jointed cleanroom wall panels with continuous seals that are compatible with the cleaning chemicals and expected temperature range. Joint sealants should be selected for adhesion, flexibility, low particle generation, and long-term resistance to cracking or shrinkage.
At wall-to-floor and wall-to-ceiling intersections, I use hygienic coving or an equivalent radiused detail where required by the room design. Coving reduces sharp internal corners that are difficult to wipe and can collect residue. The transition must remain continuous across changes in panel direction, doors, equipment bases, and service penetrations.
Penetrations are a common source of hidden compliance risk. Electrical conduits, pipes, ducts, sensors, sprinkler lines, cable trays, and process utilities should use designed sleeves, gaskets, collars, or sealed plates rather than uncontrolled site-made openings. Concealed fasteners and factory-prepared openings can reduce exposed ledges and the number of field seals that must be inspected.
Airtightness should be verified as part of the completed enclosure. Depending on the project, this can include visual seal inspection, smoke testing, pressure-decay testing, room pressure verification, or another documented leak-test method. The acceptance record should identify the test method, test location, pressure condition, result, inspector, date, and corrective action for any failed area.
GMP requirements focus on preventing contamination, mix-ups, and conditions that could affect product quality. ISO 14644 cleanroom standards address airborne cleanliness and related cleanroom performance, but an ISO classification does not automatically prove GMP suitability. FDA expectations and EU GMP Annex 1 also place emphasis on facility design, cleanability, contamination control strategy, maintenance, qualification, and documented operation.
For this reason, I treat the panel as one part of a controlled environment. Wall and ceiling systems must work with HVAC filtration, pressure differentials, air-change design, room zoning, material flows, personnel flows, and environmental monitoring. A panel with a cleanable surface cannot compensate for poor airflow balance, failed door seals, damaged filters, or uncontrolled movement between rooms.
Fire-code requirements can significantly change the panel selection. Rock wool, calcium-silicate-based boards, magnesium-based cores, PIR, PU, EPS, and honeycomb constructions may have different fire, smoke, flame-spread, and structural characteristics. I require the fire classification for the complete panel assembly and confirm that it is accepted by the authority having jurisdiction.
| Application condition | Preferred surface or core direction | Critical checks |
|---|---|---|
| Frequent disinfectant use | Stainless steel, compatible HPL, or validated coated surface | Chemical exposure, coating adhesion, sealant compatibility |
| High humidity or washdown | Stainless steel or fiberglass-facing system | Moisture ingress, corrosion, drainage, joint sealing |
| High fire-performance requirement | Rock wool or approved fire-rated board system | Complete assembly fire report and local code acceptance |
| Temperature-controlled room | PU or PIR insulation, subject to fire review | Thermal conductivity, vapor control, condensation risk |
| Lightweight ceiling or partition | Aluminum honeycomb or selected lightweight core | Deflection, support spacing, impact and service loads |
| High-impact logistics area | Reinforced facing and protected corners | Dent resistance, repair method, trolley contact points |
| Aseptic or high-grade processing room | Low-porosity facing with minimal joints | Joint continuity, penetrations, airflow and qualification |
| Cost-sensitive support room | Coated steel or selected sandwich panel | Service conditions, fire rating, cleaning chemicals |
Installation quality can determine whether a technically suitable panel remains suitable after construction. I use approved shop drawings, panel identification records, installation tolerances, sealant batch information, and inspection hold points. The installation team should understand cleanroom behavior and avoid cutting, drilling, sanding, or storing dusty materials inside completed controlled areas.
Inspection should cover panel alignment, surface damage, joint width, seal continuity, coving transitions, corner protection, fasteners, door interfaces, window frames, ceiling connections, and utility penetrations. Scratches, dents, exposed core, delamination, coating bubbles, open joints, and cracked sealant should be recorded and corrected before final cleaning. Repairs should be documented with the material used, location, date, and acceptance result.
Qualification activities may include room pressure tests, airflow visualization, air-change verification, HEPA filter integrity testing, nonviable particle classification, viable monitoring, recovery testing, temperature and humidity checks, and surface inspection. The exact tests depend on the room grade and facility validation plan. Panel inspection should be linked to the broader qualification package rather than treated as a separate cosmetic review.
HVAC integration is particularly important because pressure differences can expose weak joints and unsealed penetrations. If a room fails to hold pressure, I first check doors, transfer openings, ceiling interfaces, service penetrations, and panel joints before adjusting the air-handling system. Increasing fan capacity does not correct a defective enclosure and may increase operating cost or create undesirable airflow.
The most common panel failures are usually associated with damage, unsuitable cleaning, or poor interface control. A scratch can expose a metal substrate, create a corrosion point, or provide a location for residue accumulation. Delamination can create an internal void, compromise cleanability, and indicate moisture or adhesive failure.
Condensation is another risk when panel insulation, vapor control, room humidity, and HVAC operation are not coordinated. Repeated condensation can weaken adhesives, damage coatings, support microbial growth on adjacent materials, and degrade seals. I specify thermal and vapor-control details based on the actual temperature difference between the room and surrounding spaces.
Incompatible cleaners can cause coating softening, discoloration, cracking, swelling, or loss of gloss. The facility should maintain a written cleaning matrix that identifies the chemical, concentration, contact time, application method, rinsing requirement, and approved panel surface. Cleaning personnel should not substitute stronger chemicals without a documented compatibility review.
A practical maintenance program should include:
I compare panel systems using more than the initial purchase price. The total cost includes material, installation, sealing, inspection, cleaning labor, repairs, replacement parts, production downtime, environmental monitoring, requalification, and possible regulatory remediation. A panel that costs less per square meter may become more expensive if it requires frequent repairs or cannot tolerate the facility’s disinfectant program.
For example, a coating failure in a production room may require temporary shutdown, controlled removal of damaged material, deep cleaning, investigation, repair, and repeat qualification. The direct panel replacement could represent only a small part of the total event cost. This is why I evaluate chemical resistance, impact resistance, joint durability, fire performance, and documentation before comparing supplier quotations.
Easywall provides Clean Room Modular Wall Systems, cleanroom wall and ceiling panels, doors, windows, and related equipment for pharmaceutical, laboratory, healthcare, electronics, and other controlled environments. Its published product range includes Medisurf® panels, metallic sandwich panels, fiberglass panels, electroplated panels, and multiple core options such as rock wool, honeycomb, EPS, PU, and PIR. The company also states that its manufacturing operations include a 23,300-square-meter production base, two automated lines, an in-house laboratory, ISO 9001 and ISO 14001 certifications, and projects across more than 38 countries.
Those figures describe manufacturing capacity and company systems; they do not automatically certify a particular room as GMP compliant. For any Easywall project, I would still request the panel data sheet, fire documentation, surface and core specifications, sealant information, layout drawings, installation method statement, inspection plan, cleaning guidance, and project-specific qualification records. The final selection should be approved by the facility owner, validation team, quality unit, architect, HVAC engineer, and fire-code authority.
Before approving a panel system for pharmaceutical manufacturing, I use the following checklist:
| Acceptance area | Evidence or measurable check |
|---|---|
| Surface | Defined roughness or finish requirement, no open pores, cracks, exposed substrate, or visible delamination |
| Non-shedding behavior | Material declaration, coating stability information, and inspection after installation |
| Chemical resistance | Compatibility against every approved cleaner and disinfectant |
| Joint continuity | Continuous seal inspection, specified joint width, and documented repair procedure |
| Airtightness | Room pressure result, leak-test record, or approved equivalent |
| Penetrations | Sealed sleeves, collars, gaskets, or factory-prepared interfaces |
| Impact resistance | Design review for carts, equipment, doors, and material-handling routes |
| Fire performance | Complete assembly classification accepted by the applicable authority |
| Core suitability | Verified insulation, moisture, fire, and structural performance |
| Documentation | Drawings, certificates, batch records, installation records, inspection reports, and maintenance instructions |
| Validation support | Information required for qualification, environmental monitoring, and change control |
What Makes a Cleanroom Panel GMP-Friendly? The answer is the combination of a smooth non-porous surface, non-shedding construction, chemical resistance, durable core and facing materials, sealed joints, hygienic coving, controlled penetrations, suitable fire performance, and documented installation and validation. The panel must support the complete contamination-control strategy rather than rely on a supplier’s marketing label.
When I specify cleanroom panels for GMP pharmaceutical manufacturing, I begin with the room use, cleaning chemicals, ISO classification, GMP grade, fire code, HVAC design, and maintenance plan. I then compare surface materials, cores, joint systems, impact protection, qualification evidence, and total cost of ownership. A practical next step is to issue a project-specific acceptance checklist and require each supplier to respond with measurable technical data, drawings, test reports, and installation records before purchase approval.
Последние новости
How Cleanroom Panels Support Contamination Control?
 Sep. 23, 2026
VHP Sterilization: Panel Coating Resistance
Sep. 21, 2026 
USP <797> and USP <800> Compounding Pharmacy Cleanroom Guidelines
Sep. 21, 2026 
What to Ask Before Buying Cleanroom Panels?
Sep. 17, 2026 
The Ultimate Cleanroom Wall Panel Guide: Materials, Cores, and Coatings
Sep. 15, 2026 Наше местоположение
No.168, Ziguang Road, Цяньцзян, провинция Хубэй, КНР
Быстрый контакт
aria@easywalltec.com leo@easywalltec.comМы свяжемся с вами в течение 24 часов или звоните нам каждый день с 09:00 до 12:00
+86 139 6255 5162
Запросите смету
Технологические инновации, качество продукции - это душа предприятия, удовлетворение рыночного спроса и потребностей клиентов - это жизнь предприятия
 English
 Chinese (Simplified)
 French
 Portuguese
 Japanese